


 +44 (0)1753 548801
 sales@upm.co.uk
Pharmaceutical Conveyors
Pharmaceutical production leaves no room for contamination risk, downtime or guesswork. Which is why at UPM, we design and manufacture bespoke pharmaceutical conveyors for UK manufacturers handling tablets, capsules, blister packs, vials, bottles and medical devices, from single transfer units through to complete handling lines.
Every pharmaceutical conveyor system we build is:
- Designed to prevent cross-contamination between product batches
- Hygienic and sanitary, with surfaces that can be cleaned, disinfected and sterilised
- Built to improve throughput and efficiency across production and packing
- Engineered around your process, your product and the space you actually have
We work closely with pharmaceutical manufacturers, contract packers and medical device producers to design conveyor solutions around bespoke requirements rather than forcing a standard line to fit.

Pharmaceutical conveyor applications
We supply conveyor systems for a range of pharmaceutical and medical applications including:
- Bottle filling conveyors for liquid medicines and supplements
- Sorting and grouping of medical and pharmaceutical products
- Blister pack handling and transfer to cartoning
- Tablet compression infeed and discharge
- Weighing and rejection systems for count and weight accuracy
- Transfer conveyors linking process machinery, inspection and packing stations
Sterile conveyor systems
Our pharmaceutical conveyor belts and frames are built from high-quality stainless steel, which can be thoroughly cleaned, disinfected and sterilised without corroding or absorbing product residue. This is vital when the same line handles more than one drug or batch.
Quick-release belts mean you can remove, sterilise, and refit a belt in minutes rather than hours. For sites running multiple products through the same equipment, the biggest time saver is usually faster changeover between pharmaceutical materials.
Reducing cross-contamination
Many factories package several different drugs on shared equipment, so cross-contamination control is a design requirement. Stainless steel belts and open, accessible frame construction make sanitation faster and easier to maintain, which makes it more likely to be done properly every time.
We can also design around specific constraints such as restricted floor space, cleanroom access, wash-down requirements, labelling stations and downstream material handling.
Contact us to talk through your sanitary conveyor requirements.
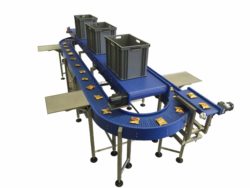
360-degree carousel and horizontal conveyor
The 360-degree carousel conveyor suits pharmaceutical packing well because it is easy to sanitise and built to last. It brings product to operators rather than moving operators around the line.
Key features:
- Transports packets of pharmaceuticals to operator stations for packing
- Central conveyor belt providing accumulation and storage
- Safe link belts
- Quick belt removal for fast clean-down
- Stainless steel support frame
- Single drive system with inverter control
- Foldable operator stations for flexible staffing
It works particularly well for seasonal or variable-demand packing, where you need to add or remove operator positions without rebuilding the line.
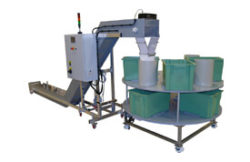
CF991 rotary box filler
Box filling conveyor systems handle the weighing and counting step, making sure the correct number or weight of items goes into every box before distribution. The CF991 slots into the pharmaceutical manufacturing process as a fast, repeatable packing stage.
Benefits of the CF991 rotary box filler:
- No specialist expertise required, press and go
- Up to 10 filling positions
- Impulse counter accepting up to 9,999 signals from the process machine
- Free access underneath the unit for storage and easier cleaning
- Plug-in frame connection attachment
- Test function on the control for position setting before automatic start
- Automated safety programme, returning to the fill position
- 240V power supply
- Stainless steel chutes, so no corrosion
- Optional clear Perspex chute cover for operator safety
Temperature control: under belt cooling fans
Many pharmaceutical chemicals and raw materials have to be held at a consistent temperature through the production line. Under belt cooling fans are built into the conveyor itself, giving you precise temperature maintenance without adding a separate stage.
- Positioned beneath the belt surface to blow ambient air onto products
- UPM advises on the number and type of fans based on your target temperature and belt width
- Temperature sensor with automatic reset
- 220V AC power supply
- Quiet running at 55dBA
- Ambient airflow of 375m³/h per fan
Our work in the medical and pharmaceutical industry
Our case studies show how our conveyor equipment has solved real problems for pharmaceutical and medical manufacturers:
- A temperature-controlled conveyor system for a UK medical device injection moulding specialist, optimising floor space and reducing waste.
- Design and manufacture of a COVID-19 test tube conveyor and rotary carousel system for Plastic Engineering Solutions in the UK.
Bespoke pharmaceutical conveyor manufacturing
Everything we supply is designed, built and supported here. Whether you need blister packaging handling, high-speed bottle filling, bulk material packing or a carousel that fits a difficult corner of an existing cleanroom, we can specify and build the equipment to suit.
Please get in touch with us with your brief, and we'll work to create the right conveyor system for you.
If you'd like to discuss any of our conveyor systems or your own requirements please call UPM on 01753 548801 or email sales@upm.co.uk.